Showing posts with label wood pellet plant. Show all posts
Showing posts with label wood pellet plant. Show all posts
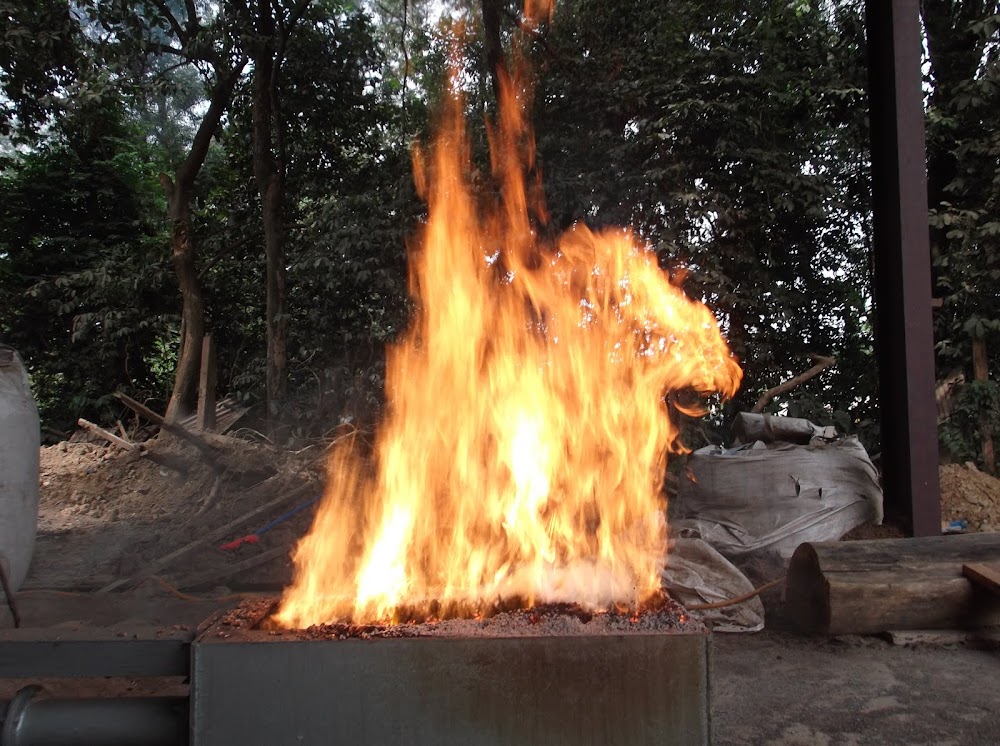
6,000,000 KCal/Hr HGG
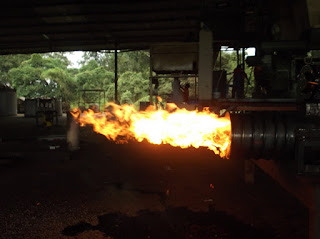
Yes this one is huge, capable of combusting 2 ton per hour of rice husk. This unit were use to supply hot gas to a ball mill in a cement plant in the Philippines.
6,000,000 KCal/Hr HGG
It is equip with sensors and inverters for control from a DCS which is 50 meter away. Only one person are posted on site and monitoring and control are carried out from the control room.
Key Features of the HGG
- 18 inch furnace wall with extra outer insulation for very low heat loss
- Automatic Deashing
- Automatic Feeding
- Inverter for FD and ID Fan
- PLC built in
- Ash Auto Mix to Ball Mill
- Over Temperature Release Vent
- and many more
PLC control in DCS
Maximum Savings of RM4,000 per hour is possible when compared to the use of fuel oil for combustion.
One of the plant we sold have a more advance furnace which reduce manpower and also ease of operation .
As pelleting need very accurate moisture content , the Hot Gas Generator help tremendously especially for big scale operation and also for less experience operator .
The Moisture Content of dust was constantly within ± 1% MC after exiting the dryer . This eliminates one of the most important varible in pelleting , in my previous post I mentioned that MC consistency are very important for good pelleting .
To explain a bit why the Hot Gas Generator helps a lot and normal furnace have it's pertinent issues . Normal furnace feeding of fuel is by hand , worker tend to overfeed the furnace which have small grate , by doing so the worker will have longer time to sit , by doing so too the temperature of the furnace will fluctuate through very wide range which cause drying inconsistency . Hot Gas Generator feed fuel automatically at set parameter and flame in furnace can be control by fan , this will give consistent flame in furnace continuously thus consistent Moisture Content of the sawdust output from dryer .
The last 6 months was hectic, nevertheless installing and commissioning them successfully was most satisfying.
Much improvement have been added to these plant which makes pelleting success a breeze, not many can claim good pelleting within few days of commissioning .
4 pellet mill
2 pellet mill
1 pellet mill in operation
If you notice the pellet quality , there is little dust and pellet was just nicely compact ( not black ) and the length is what was set by the knife ( not short or broken ). I believe those who produce this kind of pellet will have very low electricity consumption and low wear and tear on parts .
As for us , our motto is finding the " SWEETEST SPOT " . Achieving this will automatically reduce tremendous cost thus higher profit per ton .
GOOD DAY TO ALL
It have been quite some time since I last blog due to my moonlighting in a biomass power plant on top of the normal business of setting up pellet plant . After the power plant stint , much needed experience were gained and would be useful for future opportunities that would arise .
Currently we are setting up a new pellet plant with capacity of 4 ton per hour with initial target production of 1,200 ton per month . Production will increase to 2,000 ton per month within 6 month of commissioning . As we have space and electricity supply ( main factor to go big ) and possibly sufficient raw material , it is hope that capacity can be increase to 5,000 ton per month in a few years ( finger crossed ) .
The new plant with much design and engineering upgrade as compared to the old plant would cut down workers to bare minimum of 4 worker per shift for the whole line , thus pushing operation to 3 shifts would be easily achievable .
Some upgrades as below :
1 ) All conveyor are connected , no human intervention , reduce fine dust dusty environment
2 ) Use of inverter for motors to control speed when changes happens
3 ) All storage area for raw material are calculated and engineered to ensure non stop operation even though there is prolong holiday or shortage of raw material , up time per annum can be push beyond 300 days . We do not just take off the shelf design for this plant after our first plant many many problems .
4 ) many more upgrades
Lastly , any taker for our pellet please contact us at
Maybe I am not convincing enough in my statement that PELLETING is very difficult .
My records and visits to many pelleting plant , be it Wood or EFB Pellet , till todate the failure is nearly approaching 20 plant , big and small included . Definitely the number is much higher than this figure .
Potential Investor must understand the reason behind it to figure out why so many failure in this industries .
I append the major factor for the failure :
1 ) Wrong Machineries
Pelleting process need very high pressure to bind the dust back into pellet , many machineries are not able to cope with the HIGH PRESSURE and thus will be damage before it even start to really produce pellet .Talking about pressure , do you know how it work ?
Pelleting need dry dust , dryer are needed to do the job , that is why American Dryer price are in the range of USD1 Million and above , the reason is you need consistent Moisture Dust to be able to produce consistently good grade pellet , otherwise there will be no pellet at all . I doubt many understand the science of drying !!
Small Pellet Mill smaller than 500 kg / hour are a definite no no unless you are willing to put your money to burn , go calculate the returns !!!
Go look at my video on Wood Pellet Manufacturing again , look at the rate of output and then compare the price of machineries . Then go visit the supplier and look at their output to be convince .
The above are only 20% of the main factor , if you do not know about the above , please do not invest , do your homework again , don't waste the precious cash for FAILURE .
2 ) Service and Training
I did mentioned earlier about this . The machineries from China is cheap because they do not provide proper Service and Training , this cost will easily increase their pricing by at least 20% . Low price act as an inducement for potential investor , so many will jump in but end up without anyone to turn to when failure stare at them
Supplier of machineries are just supplier , I am convince many are great Marketeer , they have never run a pelleting plant before . So when the going gets tough the supplier do not get going , they just ignore you .... , sounds familiar I guess .
Supplier are from China , they are not locals , they cannot stay long to guide and train local staff , so you can guess what will happen if problems start to crop up , who you gonna call !!
3 ) Experience and Skill
Ask yourself , how much you know about Biomass and Manufacturing , I would say , if you are going to invest based on the so many inquiries you get from the market , please keep your cash in the Bank , at least it earn interest . If you do not have over few years on Material experience and few years in manufacturing it is a definite no no to invest
Do you have an enquiring and analytical mind ? Every action will have a reaction , when something happen there must be REASONS why it happen , it cannot happen just out of nothing . There is a Chinese saying , Die also don't know because of what !! I am saying this because this will happen many many times and you will need your skill and experience to overcome it
Mark my word , go check around before you really decide to invest in this industry . There are too many failure which is not good for this industry overall .
I get many calls enquiring about pelletisation of EFB ( Empty Fruit Bunch ). We did sample production many months back , it was easy for us as EFB is a single species raw material as compared to wood sawdust where the range of wood density varies widely which is difficult to control during material preparation . You can see the quality of EFB Pellet from the test run was of higher quality in terms of length and density ( Shinier ) . The tricks of getting good quality EFB Pellet is at the material preparation side . If the input quality is good and with properly setup Pellet Mill there will be no problem in pelleting EFB .
EFB Pelleting Plant is more expensive compared to Wood Pelleting Plant as material preparation section will be needed to process EFB strand into smaller particles . EFB Input can be in the form of Whole Bunch EFB or Shredded EFB . Shredded EFB is the result of EFB being pressed in Palm Oil Mill for additional oil extraction .
EFB Plant setup are therefore different from Wood Pellet Plant because of additional machineries and thus planning ahead will bring tremendous profit later .
In the case ot Shredded EFB or Pressed EFB , it need to be cut to shorter length . Thereafter , I would like to Dry it here when the EFB is in short length . But there are other ways to do this depending on your setup and dryer capability .
Material Sizing is very important before the material enter pellet mill otherwise if the strand is too long it will choke the Pellet Mill and jammed the machine . This is where the skill and experience comes into play .
Some say Flat Die Pellet Mill is better and some argue Ring Die is as good , this depends on the " DRIVER " if you get what I mean !!!
The good pellet mill is the one that give you good quality pellet and high efficiency with minimal maintenance and downtime .
" DO NOT ATTEMPT THIS STUNT WITHOUT PROFESSIONAL GUIDANCE "
There are many cases of failure to do it right from start and in the process losses are huge . Get correct advice from reputable and reliable supplier with know how to start . Many a times the seller of machineries just want to close sales and promise you the sky where in fact ( and most does ) they do not have the skill to run a pellet plant , worst if their machineries are not reliable . I have been to many plant which is a failure , my statistic , 7 - 8 out of 10 are failures or loss plenty of money before they can even start to make profit .
I have touch on this topic in December 2010 in the title of Sawdust Drying . In many cases material needs to be dried to certain acceptable Moisture Content before it can proceed to the next stage of manufacturing .
In my visits to many plant , I have seen too many mistakes made in the selection of drying system , either wrong fuel are used , wrong design of furnace , wrong design of dryer , wrong design of conveying system for input and output of materials and etc . This mistakes cause many other problems down the line especially during pelletisation not mentioning high cost of drying . Make no mistake , you cannot have good system if you do not have proper knowledge of drying and combustion . That is why drying system are expensive because it will saves you money later and in some cases a matter of do or die .
Drying Efficiency
Drying for pelleting process are normally done with direct chanelling of hot flue gas into the drum dryer where the hot air are in direct contact with the material to be dried . This process of direct contact are of highest efficiency as compared to indirect heating with a heat exchanger . Depending on material , moisture content of the material and structure of the material , the hot flue gas input temperature can be as high as 800º celcius . The higher the temperature , the faster the material are being dried and you will get higher output from the drum dryer otherwise the drying section will become bottleneck . Consistent temperature from the furnace to the dryer are also important so that the Moisture of Biomass dried is consistent . To achieve consistency and narrow range of Moisture , firing into furnace or dryer need to be consistent , this can be achieve by having good Burner .
Drying Cost
Many a times this was overlook , everything we sell have a selling price and it also come with a cost . Similarly in wood pelleting , there is cost to manufacturing of wood pellet , and to those who use wet sawdust or even EFB , there will be need for drying , this is one section which is often overlook . Good cost structure will be drying cost of below RM20 / MT of dried raw material . How do we achieve this :
1 ) use low cost material like timber offcut , woodchip , EFB , Palm Fibre etc
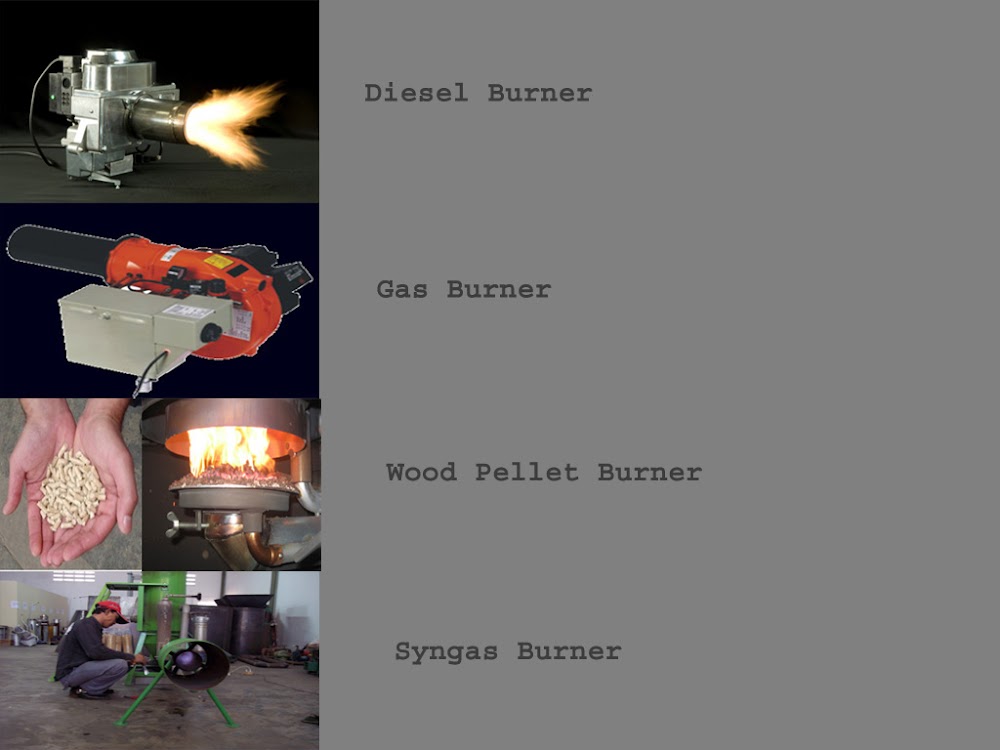
2 ) use high efficiency pellet burner because you are producing pellet
3 ) do not use electricity , gas or diesel burner , you calculate the cost yourself to find out
That being said , the planning of Good Drying System is pertinent to keep the cost low so that there will be profit in the selling of pellet . If you dry your material above RM50 / MT then this business will be unprofitable .
In short it is not easy to keep cost low as currently for any fuel there is cost involved , selection of correct drying system are important .
Drying Quality
During pelleting process , consistent Moisture Content of material input are important to give consistent quality of pellet output , otherwise one minute you will get good and the next minute bad quality pellet . Therefore dryer must have flexibility to ensure Consistent MC for biomass output from dryer .
For your information , any sawdust or even EFB will have sand and stone in it , too much of it will increase the ash content of pellet and thus pellet price will be affected . A good dryer will have system to remove partial of the sand and stone .Removal of sand and stone will also prolong the life of roller and die during pelleting process .
3 of the above factor are important in the selection of the correct dryer . Wrong selection will cause the followings :
1 ) Under or Over Capacity of dryer
2 ) Low temperature input will cause slow drying
3 ) Inconsistent temperature cause fluctuation in drying thus MC of biomass dried will not be consistent
4 ) Wrongly build furnace do not give enough heat input to dryer causing under utilisation of dryer
5 ) Wrong air flow of hot flue gas are not sufficient for drying of biomass
6 ) Wrong design of input and output conveyors reduce the efficiency of drying
7 ) Non Flexibility of dryer controller make it difficult to get good drying results
8 ) Wrong biomass used for firing , increase cost of drying , whole project not viable
9 ) Manual feeding of biomass fuel in big furnace are not recommended as labour incur cost and optimum drying are not achieved
10 ) Inconsistent MC of biomass dried cannot be pelletise into good quality pellet
11 ) Too much sand and stone will jam the Pellet Mill and damage other parts
Quality Control and Research and Development Programme
Manufacturing is define as :
The process of converting raw materials , components or parts into finished goods that meet a customer's expectations or specifications .
That being said , I would like to add , to be able to make profit the whole process is a race against time to reach optimum level of operation in shortest possible time .
As of now I believe there are more than 10 wood pellet plant in Malaysia , probably over half have difficulties in producing high quality pellet and running at low efficiencies . Some are not running at all . I admit mine are also having problems with breakdown here and there , but importantly improvement are carried out after each obstacles thus weakness becomes strength .
Wood Pelleting are more an arts rather than skill . There are just too many variables especially for China Made Machines .
Unless and until you get all the parameter right , it is near to impossible to get high efficiency and quality .
In many organisation QC and R & D are lacking especially in the SME . This is the nature of business as it is too costly to setup and followup . But without these you would be FLYING BLIND , that is what happen and the blame is simple , on the machine . No doubt , China Machine is bad but there are ways to go around to get it better . Unless you are willing to invest in American or European Machines which will cost a bomb .
In wood pelleting , the person in charge MUST be able to setup proper recording so that improvement can be carried out . Proper records are just like a GPS in a foreign country . You use it ( the records ) to see :
1 ) Who can help
2 ) What happened
3 ) Where are you now and where are you going
4 ) When can you arrive
5 ) Why things happen
6 ) How did it happen
Remember the 5 W's and H
!! GHOSTBUSTER !! SOUNDS FAMILIAR
Imagine that you are starting , you get into problem , the supplier of the machines did not give correct procedure ( friend , they are seller of machines , they will promise you sky to sell , they are not production man , how do you expect them to give full range of advice when we are paying pittance for the machines ) and your machine are damage or you are running at very low effciency .
What do you do ???
You try and try , after 2 months time loss you give up , losses amounts to RM50,000 or more , you still want to carry on but do not know where to start and when can solve all this problems . Sounds very familiar , it happen to me too !!
What do you do ??? or better WHO YOU GONNA CALL !!! GHOSTBUSTER , CALL ME .
For now enjoy the song & video .
Word of Advise , if you are not able to solve the problems in 2 months , it is not possible for me to solve it by phone , it is just impossible , there are just too many parameters and you will need tools to help just like the GPS .
With all the advice and tools hopefully you are on the way for higher efficiency and higher quality of wood pellet .
Many people called but are unwilling to pay ( no free lunch ) , so advice from the phone are limited in quality , they try the method advised still doesn't work , it won't work , we take 6 months of blood sweat and tears to perfecting our method , so with 30 minutes advise you expect it to work , I wish how simple it is .
In fact I would advise , after you have commission your machine and it does not perform to expectation within 2 weeks , better call me immediately for consultation , if not you will lose 2 months at least and over RM50,000 for trial and error .
Combustion is said to be STOICHIOMETRY when fuel and air are in perfect balance . Sounds too technical !!
In layman terms :
Stoichiometry = Perfect Combustion
i.e. Highest Heat Power output at the lowest fuel consumption .
The above graph can be easily explain as follows :
EXCESS FUEL - A lorry laden with overweight goods climbing steep hill , the driver hits the accelerator full throttle but there was no extra power only more black smoke , in such circumstances more diesel escape without full combustion in the engine thus EXCESS FUEL but no extra power . While
EXCESS AIR - In a furnace , say you need 6kg of air to fully combust 1kg of fuel ( normally biomass ) , but you input more air which is at ambient temperature of 30°C while the furnace temperature was 700°C , by channelling too much cold air into the furnace , temperature will drop and thus loss of heat energy .
Please note the grey highlight " Highest efficiency " , the graph show that it is not possible to have perfect combustion ( stoichiometry ) but always burner are design with certain % of excess air , normally 10 to 15% more air to ensure full combustion .
To achieve this , Burner design are critically important . Design of burner take into account factor as follows :
1 ) timing and quantity of fuel feeding
2 ) volume of air corresponding to fuel input
3 ) robustness of burner to ensure low maintenance
4 ) automatic control to achieve highest efficiencies
5 ) safety features of the burner
6 ) simple design but high efficiency
7 ) user friendly
Penny Wise Pound Foolish
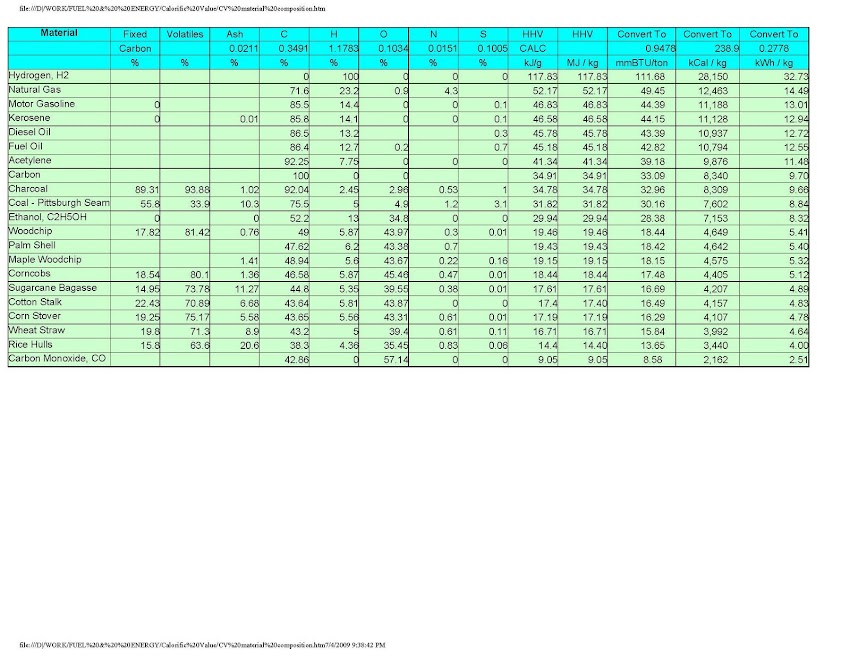
Many executives of companies do not understand this and only think of cheap material to burn in their boiler but in fact not always cheapest biomass wins hands down . Then you got to know the calorific value of the cheap biomass and also the efficiency of burning this cheap biomass . More often than not cheap biomass are very low in calorific value of not more than 2,500 kcal / kg and due to the fluctuation of the Calorific Value it is not possible to have high efficiency during combustion .
I always say this , the boiler man being normal layman will open exhaust valve fully to let more air in so no black smoke in the chimney but by doing so Excess Air will drop the efficiency to below 50% . This means instead of having good burner with efficiency over 80% there will be loss of 30% in combustion efficiency .
So the combination of Biomass Calorific Value and Combustion Efficiency might overwhelm even the cheapest biomass in terms of dollar and cents .
I hope the above will enlighten misconception on pricey biomass .
We have started manufacturing a few weeks ago and everything is going fine with small adjustment here and there . The longer than expected delay are due to testing of various materials available to us like sawdust , wood shavings and rice husk .
During testing , we encounter very big problem with local pelletising materials which we have solved . This have cost us 2 weeks delays and substantial losses . It is a journey to get the correct mix for most optimum production efficiency and yield . There is a saying ' FAILURE IS A FAR GREATER TEACHER THAN SUCCESS '
Production are now ramming up to about 1.2 ton per hour ( TPH ) per unit of Pellet Mill Model SZLH420 which is quite efficient since the supplier only promised us 1 TPH . Operation time for the machine is now 10 hours / day .
If everything is fine we will be trying to get 1.5 TPH in another month or so with 12 hours operation / day giving a total of 36 ton per day volume if raw material is available .
VIDEO - WOOD PELLET PRODUCTION
We are marketing this 2 TPH Full Production Line at RM850,000 with spare parts . Local fabrication and civil work will cost another RM150,000 or so depending on setup . We throw in service and technical advise which is the Most Important part in the setting up of wood pellet plant . Otherwise new player will have big headache in achieving optimum production within a short time .
If you notice in the video , the Plant we have are quite clean in terms of dust control even with all the machineries in operation . Some of the plant setup do not cater for dust control and in the long term it will become health hazard and difficult to maintain staff .
Costing
With this setup , we manage to bring down the total number of worker to only 8 including 2 Supervisor per shift without stoppage during tea time break and also lunch break . This is a huge savings on manpower and also during this difficulty time of getting worker . With time and additional accessories we would be able to cut another 2 worker per shift in a few months time .
Electricity consumption for the whole plant , at below 300 Ampere consumption is 125kWh of electricity which comes to RM45 / hour for a 2 TPH production . Cost of production per ton will be RM22.50 .
To achieve 1.5 TPH High Quality Wood Pellet consistently , a few problem need to be solve :
1 ) consistently stable moisture content of sawdust
2 ) particle size of sawdust
3 ) good pellet mill and accessories with proper maintenance
4 ) properly design full production line for efficient production
5 ) correct mix of tropical sawdust / rubberwood sawdust
Quality
Quality wise it is above expectation . The Certificate of Test shows that ash is below 1% and Pellet Unit Density is at 1.2 ton / m3 .
This specification is upto Germany DIN Plus Standard on Size , Unit Density , Moisture Content and Ash Content .
Like I said previously , investor need to see for themselves if it is true that the pellet mill can produce 1.2 TPH consistently and operate over long hours without stoppage .
Come visit us to see for yourself .
But no Video & Photos Allowed ( company policy ) .
Pellet Mill are the " HEART " for Wood Pellet Production , Very Important . All other equipment are Ancillaries .
Pellet Mill Equipment from China are still at a very infant stage as compared to American or European Pellet Mill , but pricing wise , it is only 1 / 5 the price .
Unless you are going for very high output and have the investment capacity to invest for very long term , China Machines are of better choice .
And even so , you have so many Suppliers , Hundreds maybe , some are Merc , some Toyotas and some Protons , you could guess what I mean , pricing starts from USD20,000 to USD50,000 / unit for a Pellet Mill and Whole Line Plant can range from USD200,000 to USD650,000 for a 2 TPH Line . We have scour many part of China for the right machines .
The lower range will get you to do more maintenance and lower production and the higher range might not be feasible for Malaysia Environment . So , choose wisely .
Due to it's infancy , choosing the right Pellet Mill are important as it have the following problems that need to be address :
1 ) Die Chamber too Hot thus Die will break under stress ( Die cost RM6,000 / unit )
2 ) 24 hours operation not possible
3 ) Standard Die size of 420mm Diameter ( the normal Model SZLH420 MZLH420 ) definitely cannot produce more than 2 TPH per machine , if all conditions are right maybe you would get 1.5 TPH , this is where the learning curve start , how soon can you achieve optimum production , simple calculation , shortage of 0.5 TPH X 2 machine X 16 hour / day X 26 day / month X 3 months X RM100 / ton = RM124,800 in Sales Value , so imagine the savings if it is longer than 3 months . ( Some Manufacturer are claiming above 2 TPH , even 3 TPH )
The Pellet Mill we chose have somehow resolve partially some of the above problems with the right combination of ancillaries equipment . In our opinion it is of reasonable pricing and technically capable to handle over 2 TPH wood pellet production with minimum staffing .
You are invited to visit us once production starts .
The problem above may need another 5 years to solved as the supplier of this machines learn from mistakes and improved on it .
Our target is to invest in reasonably priced machine , high efficiency and low maintenance , so that we can recoup our investment in shortest time possible and have a decent profit to show .


 The lower range will get you to do more maintenance and lower production and the higher range might not be feasible for Malaysia Environment . So , choose wisely .


 Posts